The drawing is the contract.
We build to the dimensions, tolerances and finishes on your drawing. Where something is unclear, we ask before we cut.
Precision CNC machining and mechanical fabrication, with a head office in Rawalpindi and a factory in the RCCI Industrial Estate, Rawat.
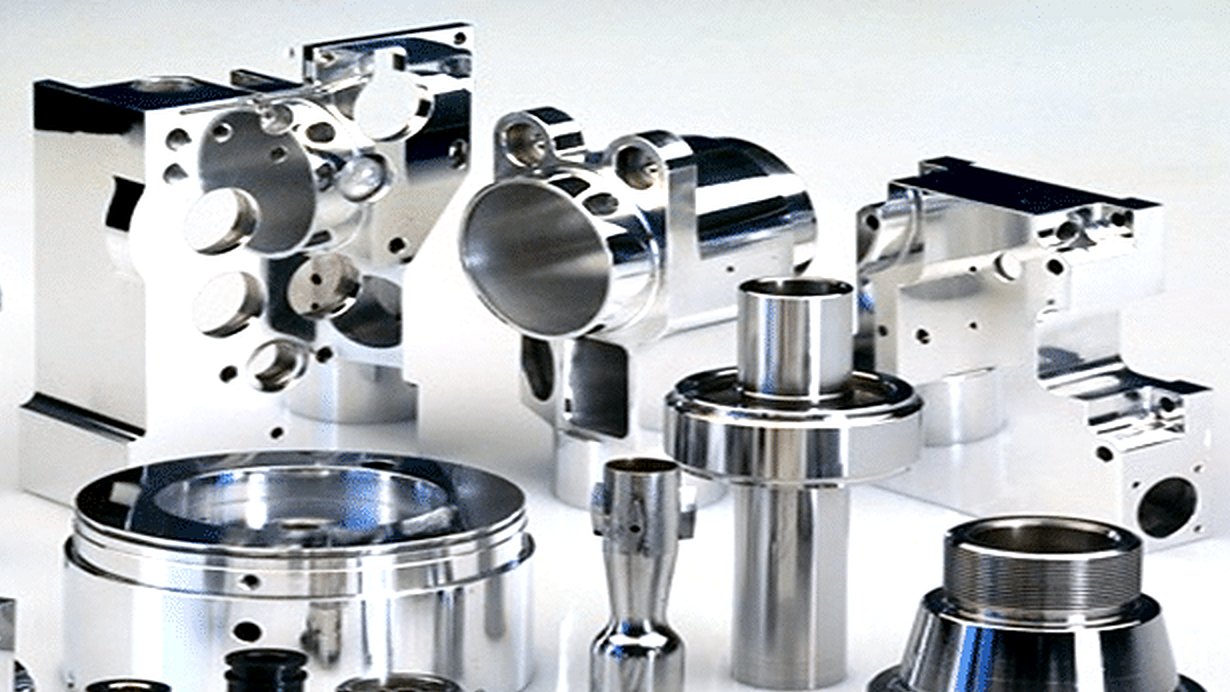
AEM Technologies is a precision CNC machining and mechanical fabrication company based in Rawalpindi, with its production facility in the RCCI Industrial Estate, Rawat. We machine components, sub-assemblies and fabricated structures to customer drawings, from single prototypes to repeat production batches. Our production hall is built around 4-axis CNC machining, supported by turning, drilling, fabrication and assembly. Every job starts with a drawing review and ends with an inspection.
We build to the dimensions, tolerances and finishes on your drawing. Where something is unclear, we ask before we cut.
First-off parts are inspected before production runs. Finished parts are inspected before dispatch.
Material is logged against its mill certificate and heat number on arrival, and stays identified through every operation.
To be the machining partner engineers in Pakistan trust first, for parts that fit at first assembly and arrive exactly as drawn.
To machine and fabricate precision parts to the drawing, on time and in full. We review every drawing before we quote, trace every bar from mill certificate to dispatch, and inspect first-off and final. Every part leaves our factory measured, documented and ready to fit.
Quality is not a department at AEM. It is built into the route card, and the records follow the part.
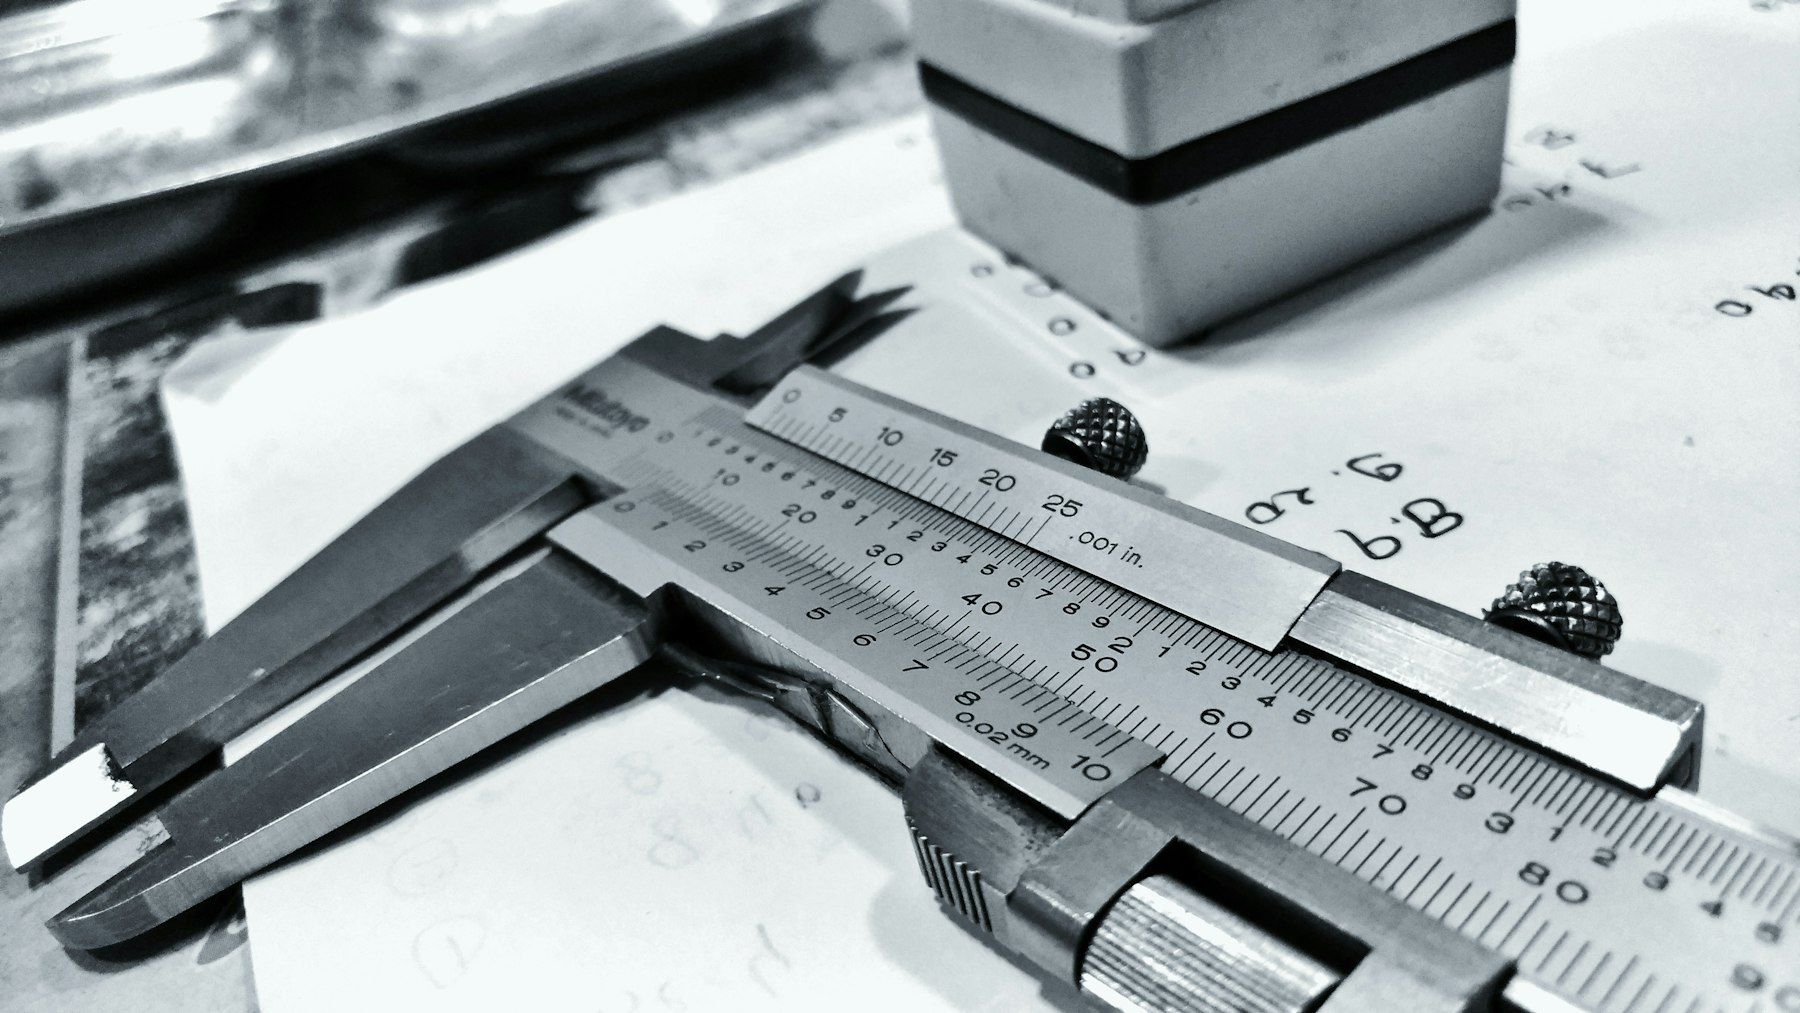
Tolerances, finishes, threads and materials are reviewed before quoting. Unclear features are raised as technical queries, not guessed.
Incoming material is checked against its mill test certificate. Heat numbers are recorded and carried through to dispatch.
The first part of every batch is fully inspected against the drawing before the rest of the batch runs.
Critical dimensions are measured at set intervals during production, so drift is corrected before parts go out of tolerance.
Threads are checked with plug and ring gauges. Bores and fits with go/no-go and bore gauges.
Every batch is inspected before release. Inspection reports and material certificates are supplied on request.
Tell us the grade on your drawing. If you are unsure, we will help you choose.
| Material | Common grades | Machining note | Typical uses |
|---|---|---|---|
| Aluminium | 6061-T6, 6082-T6, 7075-T6, 2024-T3, 5083 | Machines fast and clean; heat and clamping controlled to prevent distortion in thin walls. | Housings, manifolds, enclosures, brackets, heat sinks |
| Stainless steel | 304/304L, 316/316L, 303, 410, 17-4PH | Work-hardens readily; sharp tooling, steady feeds and rigid set-ups for clean finishes. | Food and pharmaceutical parts, fittings, shafts |
| Carbon & alloy steel | S275/S355, EN1A, EN8, EN19, EN24, 4140 | Predictable and versatile; machined annealed or pre-hardened, finished after heat treatment. | Shafts, gears, pins, flanges, hydraulic parts |
| Tool steel | D2, O1, H13, P20 | Machined annealed with allowance, then hardened; critical features finished after. | Dies, punches, jigs, wear parts |
| Brass | CZ121, CZ108, CZ112 | Free-machining and stable; clean threads and bright finishes with minimal burr. | Fittings, bushings, pins, valve parts |
| Copper | C101, C110, C103, CuCrZr | Soft and gummy; sharp polished tooling and generous coolant to avoid smearing. | Busbars, electrodes, terminals, thermal parts |
| Engineering plastics | Acetal (POM), PA6/PA66, PTFE, UHMW-PE, PEEK | Heat sensitive; light cuts, sharp tools and careful fixturing hold size. | Bushes, wear strips, insulators, food-contact parts |
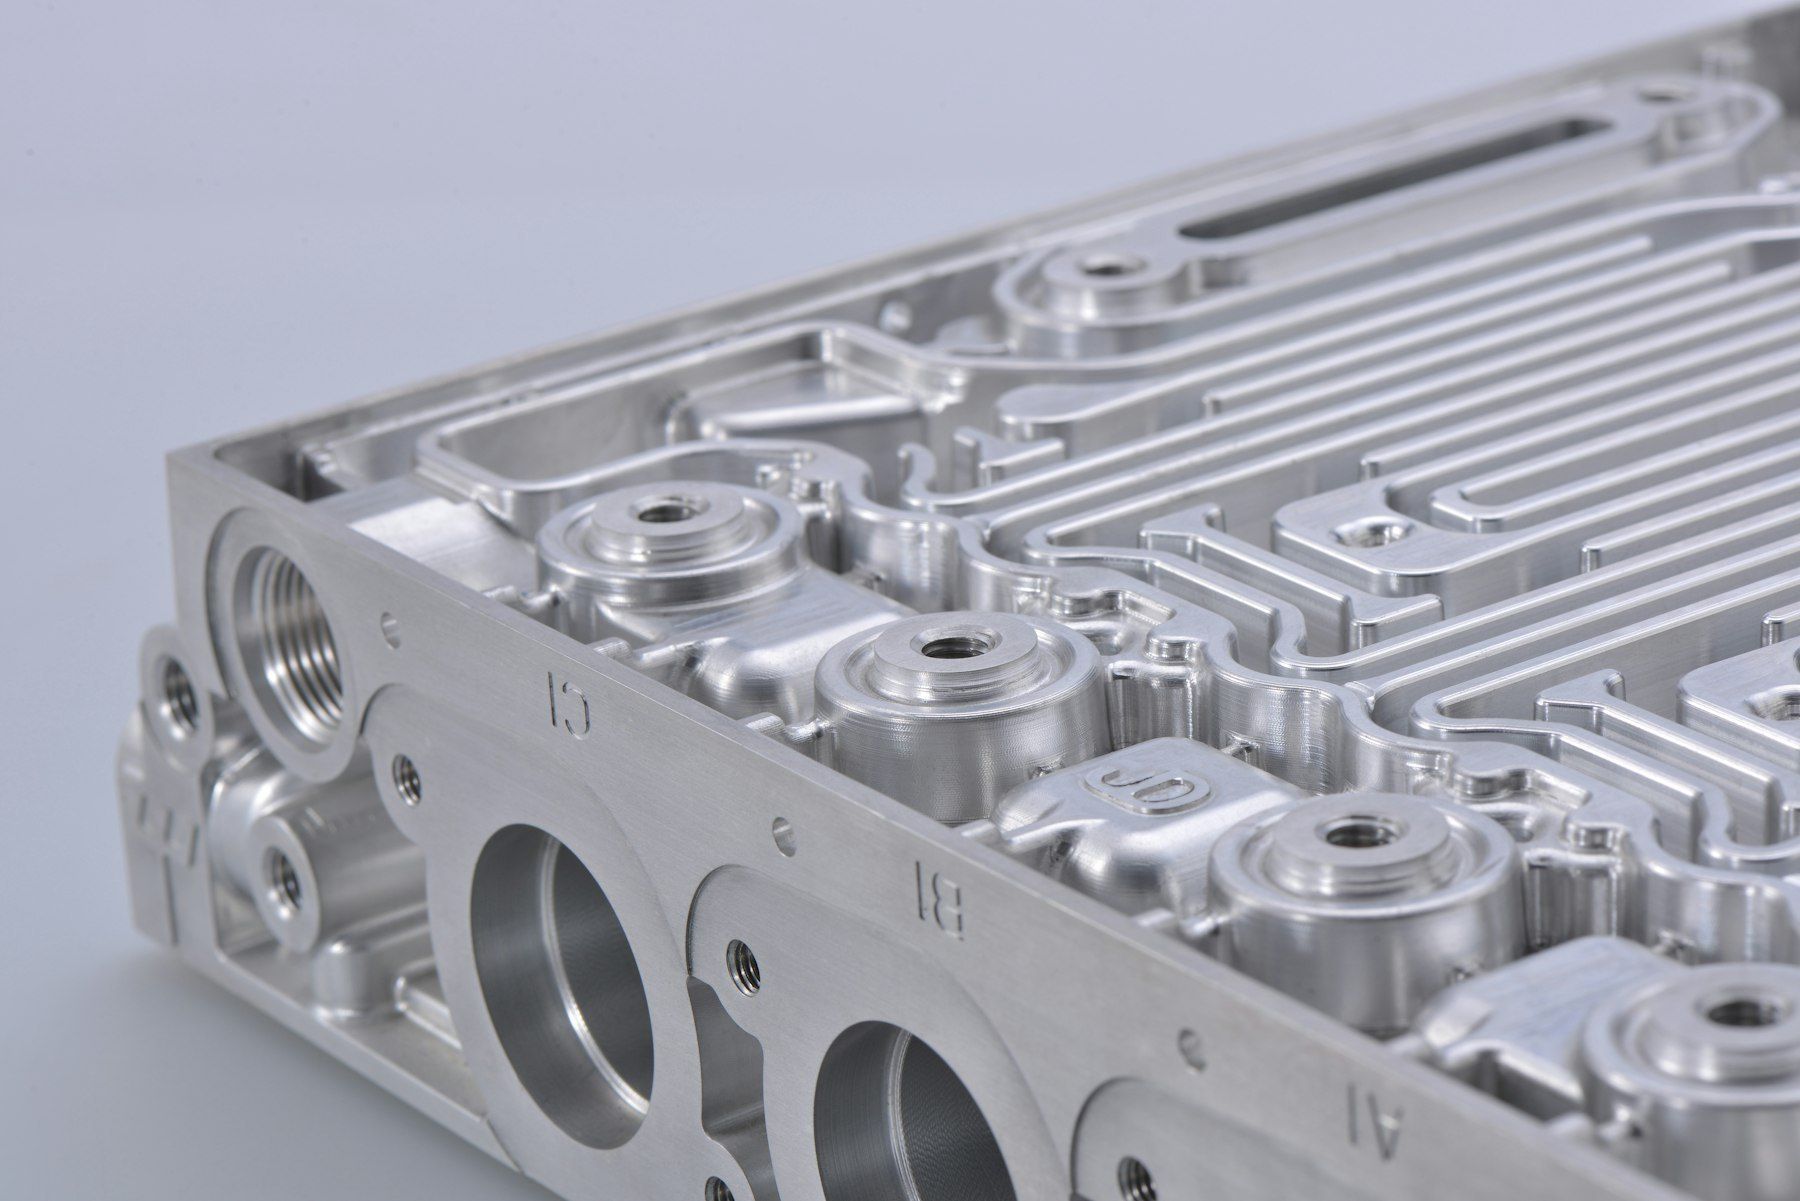
PDF, DWG, DXF, STEP or IGES. We review it, ask what needs asking, and come back with a price and a lead time.